


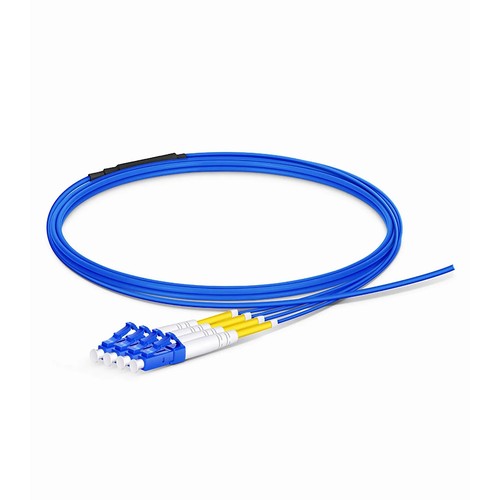
For Nigerian deployments, this product should be evaluated as part of the complete network path, including its connectors, mapping and acceptance values. This made-to-order pigtail platform is built to the ordered configuration: OS2 fiber mode, connector family, polish, jacket rating and length are all confirmed before the build starts. Each leg is factory terminated, polished and optically tested, which means the splice point inherits a connector end face that field polishing cannot match. The armored construction adds crush and rodent protection for routes that leave the safety of the tray.
Product Highlights
- Stainless Steel Tube Provides Additional Crush and Rodent Protection
- Customized 2-24 Fibers Pigtails Are Serialized for Traceability
- Optical Testing Guarantees Insertion Loss and Returns Loss
- Riser (OFCR)/LSZH Flame-retardant Jacket with Tight-buffered Coating on Each Optical Fiber
- Available with LC, SC, FC, ST, LSH Connectors
Specifications
| Connector A | LC/SC/FC/ST/LSH UPC/APC Simplex |
|---|---|
| Connector B | Unterminated |
| Fiber Count | 2/4/6/8/12/24/48 Fibers |
| Fiber Grade | G.657.A1 |
| Fiber Mode | OS2 9/125μm |
| Wavelength | 1310/1550nm |
| Breakout Length | 0.3/0.5m |
| Cable Jacket | Riser (OFCR)/LSZH |
| Min. Bend Radius (Fiber Cable) | 10/5D (Dynamic/Static) |
| Tensile Strength (Long/Short Term) | ≥200N,≥400N |
| Attenuation at 1310nm | 0.36dB/km |
| Attenuation at 1550nm | 0.22dB/km |
| Insertion Loss | ≤0.3dB |
| Return Loss | UPC≥50dB, APC≥60dB (LC/SC/ST/FC) |
| Operating Temperature | -20 to 70°C (-4 to 158℉) |
| Storage Temperature | -40 to 80°C (-40 to 176℉) |
From raw fiber route to documented port
Each structured cabling plant ends the same way: a cable arrives at a frame, and its fibers must become ports. The pigtail is the component that makes that conversion. Spliced into a tray and presented on a panel, every strand gains a connector with a known optical signature, a position in the documentation and a place in the test record. That conversion - cable to port - is where link quality is won or lost.
Mechanical splicing as the field fallback
Where a fusion splicer cannot be considered available, mechanical splices get the link up: the strand cleaves, seats in the mechanical splice body and locks against the field fiber. The loss is higher than a fusion joint and the reflectance worse, which means the practice is a fallback rather than a standard - but for urgent restoration work a pigtail that supports the two methods keeps the option open.
Ordering a customized pigtail platform
The made-to-order platform turns a catalog of options into one ordered configuration: connector family from LC, SC, FC, ST and LSH; polish as UPC or APC; jacket rating to suit the route; length to the measured run; and fiber count where the platform offers it. State the combination with the enquiry and the factory confirms the manufacturable specification before the build starts. The delivered pigtail then matches the rack panel hardware, the tray geometry and the route without field improvisation.
Configuration choices that matter at the tray
Three choices decide how a made-to-order pigtail behaves at the splice point: the interface connector family must correspond to the rack panel adapters, the polish discipline must correspond to the plant - mixing UPC and APC at one mating point destroys return loss - and the jacket rating must satisfy the pathway code. Getting these right at order time is faster than any field correction, and the factory test report then applies to the exact delivered configuration.
Armored pigtails for exposed routes
Standard 0.9mm strands survive inside trays and enclosures; routes that cross open trays, cabinet floors or retrofit pathways need more. The armored constructions wrap the fiber in helical steel - and in the industrial versions a TPU jacket - adding crush resistance, rodent protection and abrasion tolerance while keeping the completed product flexible enough to dress. The splice end still presents a standard prepared strand, which means tray practice does not itself change.
Bend-insensitive glass in dense trays
Splice trays and panel rear spaces punish fiber: tight routing, crowded dressing and the occasional hurried re-entry all bend strands beyond what legacy single-mode tolerated. The bend-insensitive grade used in this pigtail holds attenuation stable at bend radii that would fog conventional glass, which keeps the link margin intact after the tenth tray opening, not just at commissioning. For Nigerian deployments, retaining this detail with the acceptance records supports consistent maintenance.
Sparing and kit planning for termination work
Pigtails belong in the termination kit in counted sets with spares: strands break, connectors get contaminated beyond recovery, and a missing spare converts a ten-minute task into a second visit. Plan one spare set per frame position, keep spare strands capped and bagged, and record which set went into which tray so replacement stock can readily be ordered to the identical specification.
A splicing workflow that scales
Productive termination crews work to a fixed routine: mount the tray, dress the cable assembly, splice the pigtails color by color, protect every joint, test every completed port, then close and label. With the routine fixed, a two-person crew terminates a full frame position in a predictable time, and the test record maps cleanly onto the documentation. The consistency also makes quality auditable - same materials, same sequence, same pass criteria across each site.
Selecting the right pigtail for the job
Five decisions define the order: the interface connector family must correspond to the rack panel, the polish must correspond to the plant, the fiber mode must correspond to the cable assembly, the construction must correspond to the route, and the count must correspond to the tray capacity. Getting all five right at order time is what turns a box of strands into a dependable termination. Where the requirement sits outside the standard configurations, the made-to-order platforms cover the remaining combinations.
Inspection and Test Procedures
Each pigtail is optically tested before packing: insertion loss and return loss are verified on every terminated leg, and the ferrule end faces are inspected for scratches and contamination. The strands ship coiled, capped and bagged, with the test results available on request.
Ordering Information and Support
Refer to this pigtail by connector, polish, fiber mode, fiber count and construction at the request stage a quotation. For configurations outside the listed options - mixed connector families, jacket ratings, lengths or project packing - send the requirement with the enquiry and the factory will establish the manufacturable specification. For Nigerian orders, our team can check the requirement before coordinating manufacture and international delivery.


